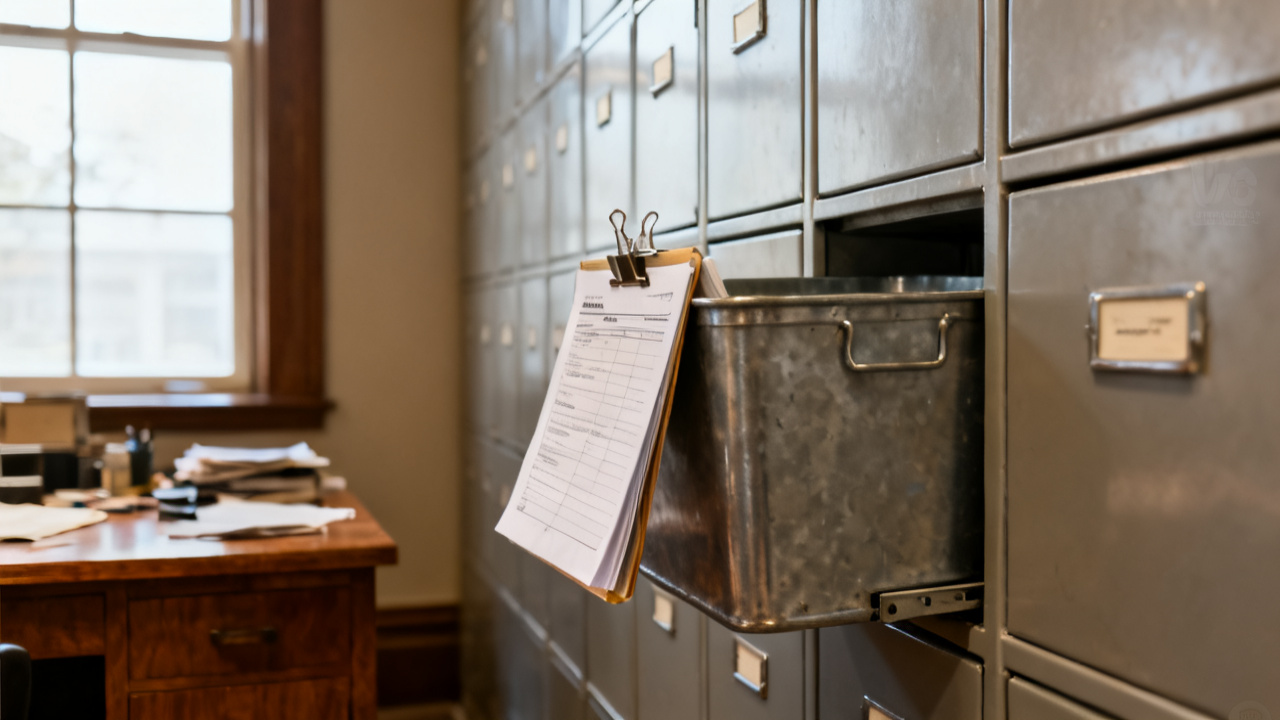
Two packets are on the same bin. The part numbers are not the same. You spot them when you slide the 12-gauge stainless steel bin out of the kitting rack for your first run of the shift. Both are sealed in clear zip-top pouches clipped to the bin’s front lip, no obvious notes flagging which applies to the 72 units you’re scheduled to deburr and laser etch today. You set your calipers down on the Traveler Desk edge to untangle the clips before you move the bin to your work holding fixture.
Active traveler matches the 3/8 NPT brass fitting lot you are running today
You cross-reference the part number printed on the traveler’s top right corner with the work order posted to your station, and the numbers align exactly. This packet includes the etching schematics, deburr tolerance specs, and lot tracking number you need to log every 12 units as you work through the lot. You clip this traveler to the side of your workbench within easy reach, so you can jot down run times and tool change notes as you go, no need to lean over to the bin every time you need to reference a spec. Illustrative example: You mark the 0.002 inch maximum outer edge burr tolerance on your workstation whiteboard to avoid squinting at the small print mid-run, since you know you will be running back-to-back units for the next three hours and small distractions can lead to out-of-tolerance parts. You also note the required etch depth of 0.005 inches on the whiteboard, so you can adjust your laser power if you notice the etch is not showing up as deep as required on the first few units. The traveler also has a small pocket on the back that holds any scrap tags you need to fill out if you pull a unit that has a crack, mis-thread, or other defect that keeps it from moving to the next stage of production. You keep a stack of blank scrap tags in your workbench drawer, but you tuck one extra from the traveler pocket into your apron just in case you run out mid-run.
Included cert links to the low-volume custom stainless adapter lot on the bin’s lower shelf
The second packet holds the material cert for the 18 custom adapters stacked on the bin’s lower shelf, which is slotted for your next run after you finish the brass fittings. You don’t need to open this packet now, but you leave it clipped to the far right of the bin lip so it doesn’t get mixed with the active traveler while you work. The cert lists the heat number for the stainless stock used to machine the adapters, which you will cross reference with your etch layout when you start that run, to make sure the heat number is etched legibly on the flat face of every unit. The cert also lists the original mill batch number, which the quality team will reference if any of the adapters fail pressure testing later in the production process, so it stays sealed in its pouch until you are ready to log the heat number for the first piece inspection. You double check that the pouch is fully sealed before you push the bin into place next to your workbench, so no cutting oil or metal shavings get inside and smudge the printed information on the cert.
Printed first piece inspection log maps to both lots to cut down on duplicate check work
The back of the active traveler has a detachable first piece inspection log that works for both lots, since both require the same deburr, etch clarity, and dimensional check steps. You fill out the top section with today’s date, your employee ID, and the bin location number before you run your first brass fitting, then follow these steps in order for each lot’s first unit:
- Run the first unit through your deburr wheel for exactly 12 seconds per edge, applying light even pressure to avoid grinding away too much material, then use your digital calipers to measure all outer and inner edge tolerances, marking each measurement in the corresponding row of the log.
- Load the deburred unit into your laser etcher fixture, making sure it is seated fully against the back stop to avoid misalignment, run the pre-loaded etch program for the lot, then check that all text and marks are crisp, no blurring or missed etching on any surface.
- Hold the unit under the station’s 10x magnifying lamp to check for micro-cracks along threaded edges, wiping away any residual cutting oil with a lint-free cloth to get a clear view of the metal surface.
- Sign and date the first piece section of the log, then flag down the on-duty quality tech to review and sign off before you run the rest of the lot, so you don’t waste time running out-of-tolerance units if you missed a spec during your initial check.
- When you switch to the stainless adapter lot, repeat steps 1 through 4 for the first adapter, using the blank second section of the same log to record your measurements, adjusting your deburr time slightly to account for the harder stainless material if needed.
This shared log cuts down on the amount of paperwork you need to file at the end of the shift, and ensures all lot data is stored in the same place for the production team to reference later if any questions come up about the run. You tuck the log back into the traveler pocket until you finish prepping your first brass fitting for the run, making sure it is fully tucked in so it doesn’t blow out when the shop’s overhead fans kick on later in the afternoon.
When you pull this packet for post-run quality signoff
You will not open the full traveler packet again until you finish running all 72 brass fittings and 18 stainless adapters, and you are ready to submit all units for final quality review. At that point, you will attach the completed first piece inspection log to the front of the traveler, tuck the material cert for the stainless adapters into the pocket on the back of the packet, and add a single sticky note to the front noting how many total units you ran, if you had any tool changes mid-run, and if any units were scrapped during production. You will not mark any units as passing or failing on the traveler itself, that step is reserved for the quality team that reviews every unit before it moves to the packaging station. You will also cross-check the lot numbers on the traveler and cert with the numbers etched on every 12th unit, to make sure no units from a different lot got mixed in with your run during the kitting process. You will count all completed units twice to make sure the number matches the total listed on the work order, minus any scrapped units you logged on the scrap tags tucked into the traveler’s back pocket. Once you have all the paperwork assembled, you clip the full packet back to the front of the bin, making sure both the traveler and cert are secured tightly so they don’t fall off when the bin is moved to the quality review holding area near the back of the shop floor. You add a small dot of blue marker to the top corner of the traveler to signal that both lots in the bin are fully processed and ready for review, which helps the quality team prioritize bins that are ready for signoff over those that are still in production. You wipe any stray metal shavings off the front of the pouch before you roll the bin away, so the quality team can read the lot numbers at a glance without needing to clean off the cover first.