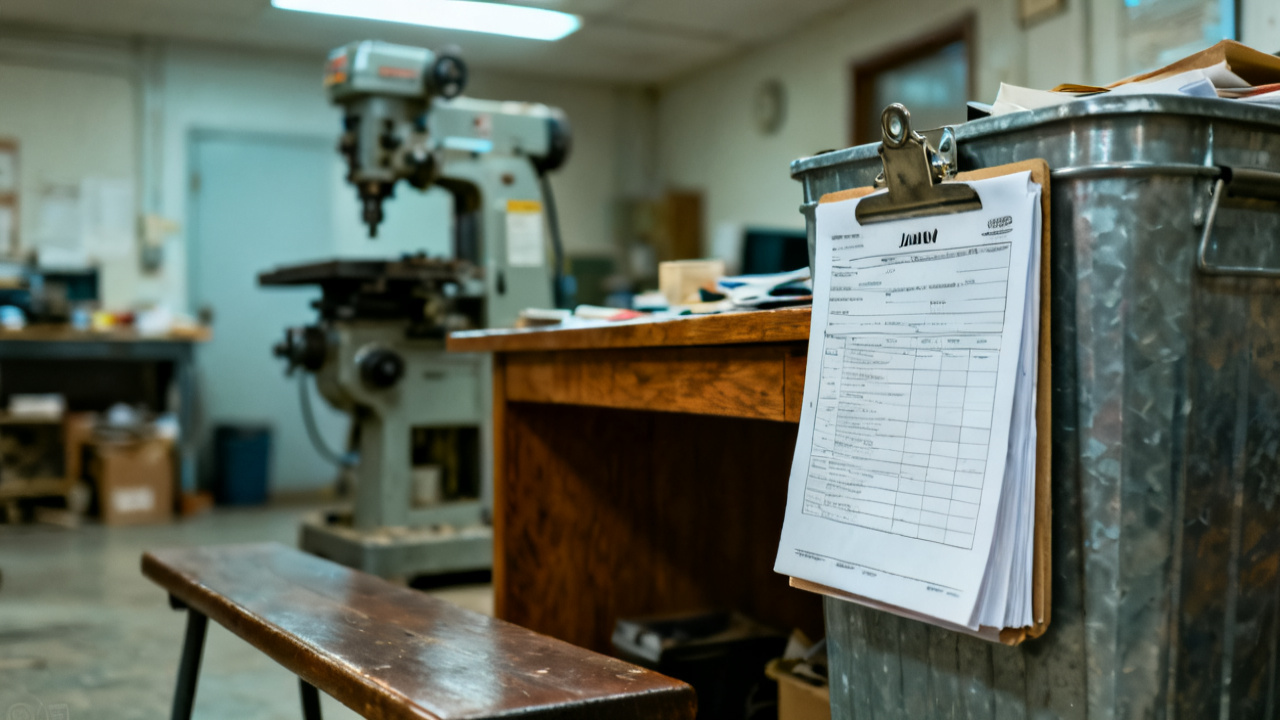
A work-instruction number is printed. The binder at the machine has another number. You pause mid-tool change, holding the sealed plastic packet you pulled from the incoming parts bin, to cross-reference both numbers against the scrawl on your bench edge for this run. You already wiped the oil smudge off the packet’s printed number ten seconds earlier, so there’s no risk of misreading a 7 as a 1.
How this document aligns number sets for the current lot
You use this sheet to cross-reference three separate number sources for every lot you run, no exceptions. The work-instruction number on the packet links directly to the specific tooling, feed rate, and tolerance settings for the parts you are machining right now, while the binder number at the machine references the master run guide for the entire part family. You avoid mixing these up, as even a single digit mismatch leads to out-of-spec parts, wasted stock, and unplanned downtime for rework. Illustrative example: 327-419-AB is the correct work-instruction number for the 6061 aluminum flanges in your current lot, while the binder number for the entire flange family is 782-001. You cross-reference both against the master number list posted at the Traveler Desk if you spot any ambiguity, to confirm you are working from the most up-to-date specifications for the lot.
Steps to verify the number matches before you run the first part
You follow this sequence every time you start a new lot, even if you ran the same part last week, to account for unannounced engineering updates:
- Peel back the top left corner of the packet’s plastic seal to expose the full printed work-instruction number, making sure you do not tear the label or smudge the ink with your work gloves.
- Flip to the tabbed section of the machine binder marked “Current Lot Specifications” and locate the work-instruction number printed at the top of the first page of that section.
- Compare each segment of the two numbers one at a time, starting with the three-digit prefix, then the three-digit midsection, then the two-letter suffix, to catch any partial mismatches that are easy to miss at a glance.
- Hold the packet next to the machine’s control panel to confirm the number programmed into the active run file matches both printed numbers exactly.
- Initial the top right margin of this sheet immediately once you confirm all three number sets are identical.
You take an extra 10 seconds for this check, even if the lot is marked as a priority rush run, to avoid costly errors that delay delivery far longer than the short verification pause.
Where you mark discrepancies on the sheet if numbers do not align
You use the lined section on the lower left third of this sheet to note every detail of any mismatch you find during your verification check. You write down the full number from the packet, the full number from the machine binder, and the full number programmed into the control panel, along with the time you spotted the discrepancy and the lot number printed on the outside of the parts bin. You flag the sheet with the neon pink sticky note you keep in your bench apron pocket, so any other team member who approaches the station before you return knows the run is on hold until the number mismatch is resolved. You leave the parts packet and binder open to the relevant pages as you head to notify the production lead, so they can cross-reference the numbers themselves without hunting for documentation. You do not make any edits to the programmed control number or the binder pages on your own, as only the engineering and production planning teams are authorized to update official run documentation.
Fields you fill out once you confirm the correct number is in use
You fill out the three pre-printed fields on the top third of this sheet before you load the first blank part into the machine chuck. The first field asks for the lot number from the parts bin, which you copy exactly as it is printed, including any leading zeros at the start of the number sequence. The second field asks for the time you completed your verification check, which you write in 24-hour format to avoid confusion between morning and evening shifts. The third field asks for your machine station number, which you note as 14B if you are working at the horizontal mill, or 09C if you are working at the vertical lathe. You also jot any minor notes about the number check in the blank margin below these fields, like if the binder number was printed slightly faded but still legible, to give context to anyone who reviews the sheet later. You do not leave any of these fields blank, as missing information breaks the traceability chain for the lot.
Information you pass to the quality tech when they stop by your station
When the quality tech comes by to check the first run part, you point to this sheet first to confirm you completed the number verification check before starting the run. You walk them through the three number sources you cross-referenced, and point to your initials in the top right margin to prove you signed off on the match. You share any notes you jotted about faded print or minor labeling inconsistencies on the packet, so the tech can flag those issues for the production planning team if they appear across multiple lots. You also hand them the parts packet so they can cross-reference the work-instruction number against the part specification sheet they carry with them for their audit. You do not start running full production until the tech confirms the number alignment checks out, to avoid wasting stock on an incorrectly programmed run.
Next shift’s first check of this lot’s matched number documentation
The operator starting the next shift pulls this sheet from the clip on the machine guard first when they arrive at the station, before they touch any controls or load any new parts. They cross-reference the work-instruction number you wrote on the sheet against the current programmed number on the control panel, the number in the machine binder, and the number on the parts packet, to confirm no changes were made during the shift handoff that would alter the run specifications. They add their own initials next to yours in the top right margin once they confirm the numbers still match, to document their own verification check. If the lot is not complete by the end of their shift, they leave the sheet clipped to the machine guard for the following shift, so the verification chain remains unbroken for the entire duration of the run. Once the last part of the lot is machined and passes all quality checks, the sheet is filed in the production records bin by the exit door, for future reference if any questions about the lot’s specifications come up later.